


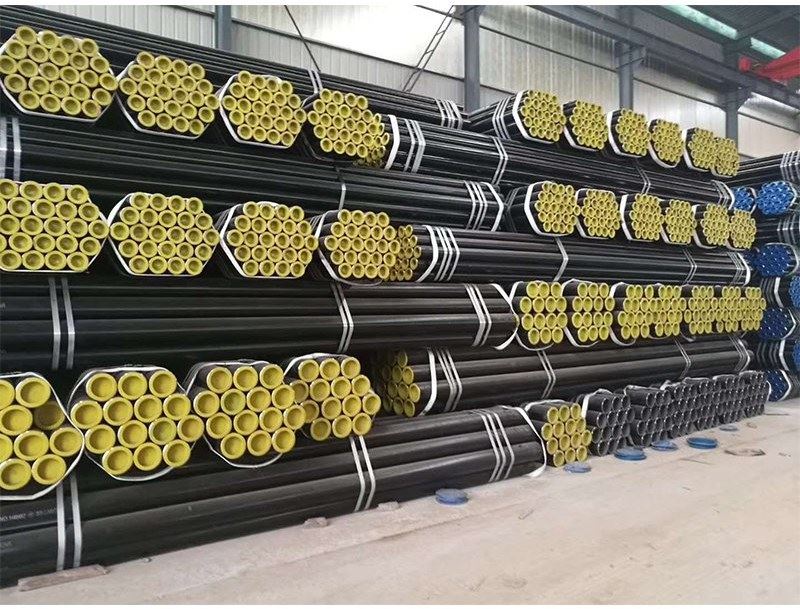
Product Overview
X70 is the workhorse grade of the middle of the API 5L strength range: 70,000 psi minimum yield, sitting between the X65 used for most distribution and gathering lines and the X80 specified for long, high-pressure transmission mains. It is chosen when a pipeline needs higher pressure or a thinner wall without moving to a grade whose weldability and toughness are harder to guarantee.
PSL2 is the part buyers underestimate. PSL1 only fixes chemistry and tensile properties. PSL2 adds carbon equivalent limits, notch toughness tested at a specified temperature, dimensional tolerances on diameter, wall and ovality, and NDT of the weld. For a gas transmission line, those extra requirements are what make the pipe weldable in the field and resistant to running fracture.
We supply X70 PSL2 in ERW, LSAW and SSAW construction, 4 to 48 inch, with 3LPE, FBE or bare finish, and with HIC and NACE MR0175 options where the service is sour.
Key Advantages
- PSL2 as standard. Carbon equivalent, impact toughness and dimensional tolerances are certified, not assumed.
- Grade-to-grade fit. X70 sits between our X65 and X80 lines, so a project can be supplied across its full pressure range.
- Weld process choice. ERW for smaller diameters and speed, LSAW for larger diameters and heavier walls, SSAW for long runs.
- Sour service options. HIC testing to NACE TM0284 and SSC to NACE TM0177 when the line carries wet H2S.
- Coating in one order. 3LPE, 3LPP or FBE applied and inspected before shipment.
Technical Specifications
| Parameter | X65 PSL2 | X70 PSL2 | X80 PSL2 |
|---|---|---|---|
| Yield strength | 65,300–76,900 psi | 70,300–82,700 psi | 80,700–93,900 psi |
| Tensile strength | 77,500 psi min | 82,700 psi min | 91,400 psi min |
| Outside diameter | 4–48 in | 4–48 in | 8–48 in |
| Wall thickness | 4.8–25 mm | 4.8–25 mm | 6–25 mm |
| Manufacture | ERW / LSAW / SSAW | ERW / LSAW / SSAW | LSAW / SSAW |
| Impact test | 0 °C or as ordered | 0 °C or as ordered | -10 °C or as ordered |
| Coating | 3LPE / FBE / bare | 3LPE / FBE / bare | 3LPE / FBE / bare |
Step-by-Step Manufacturing Process
- Plate / coil selection. Heat chemistry adjusted for carbon equivalent, which controls field weldability.
- Forming. ERW for smaller diameters; LSAW or SSAW for larger.
- Welding. Seam welded with parameters recorded; weld zone heat treatment where the specification requires it.
- Sizing. Diameter and ovality set to PSL2 tolerance, ends machined square.
- Testing. Hydrostatic test, weld NDT, and Charpy impact at the specified temperature.
- Coating. Surface preparation, then 3LPE, 3LPP or FBE with holiday and adhesion checks.
Quality Assurance & Certificates
- EN 10204 3.1 certificate per heat: chemistry, carbon equivalent, yield, tensile, elongation
- Charpy impact results at the ordered test temperature, per weld and per body
- Hydrostatic test report per pipe
- Weld NDT records - UT, radiographic or both
- HIC / SSC test reports for sour service orders
- Coating report: thickness, holiday test, adhesion
Core Applications
- Gas transmission pipelines - the main use of X70
- Crude and product lines where higher pressure reduces wall thickness
- Gathering and trunk lines in oilfield development
- Compressor and metering stations - short spools and manifolds
- Water and slurry lines at high pressure, where abrasion is not the governing factor
FAQ
Why X70 rather than X65?
Higher yield allows a thinner wall at the same design pressure, which reduces steel weight and welding time over a long line. The trade-off is tighter chemistry control - which is exactly what PSL2 certifies.
Do you supply sour service?
Yes, with HIC testing to NACE TM0284 and SSC testing to NACE TM0177, plus hardness limits on the weld. Sour service must be stated at enquiry stage, not added later.
What coating should I choose?
3LPE for buried lines in most soils, FBE where operating temperature or mechanical damage risk favours a thin film, 3LPP for higher temperatures. Concrete weight coating can be arranged for subsea or buoyancy-controlled sections.


Frequently asked questions
What are the main technical parameters of API 5L X70 Line Pipe?
Yield strength: 65,300–76,900 psi; Tensile strength: 77,500 psi min; Outside diameter: 4–48 in.
Which industries use API 5L X70 Line Pipe?
Gas transmission pipelines - the main use of X70; Crude and product lines where higher pressure reduces wall thickness; Gathering and trunk lines in oilfield development.
What quality documents accompany API 5L X70 Line Pipe?
EN 10204 3.1 certificate per heat: chemistry, carbon equivalent, yield, tensile, elongation; Charpy impact results at the ordered test temperature, per weld and per body.


